

What are the requirements for the surface roughness of the blister mold?
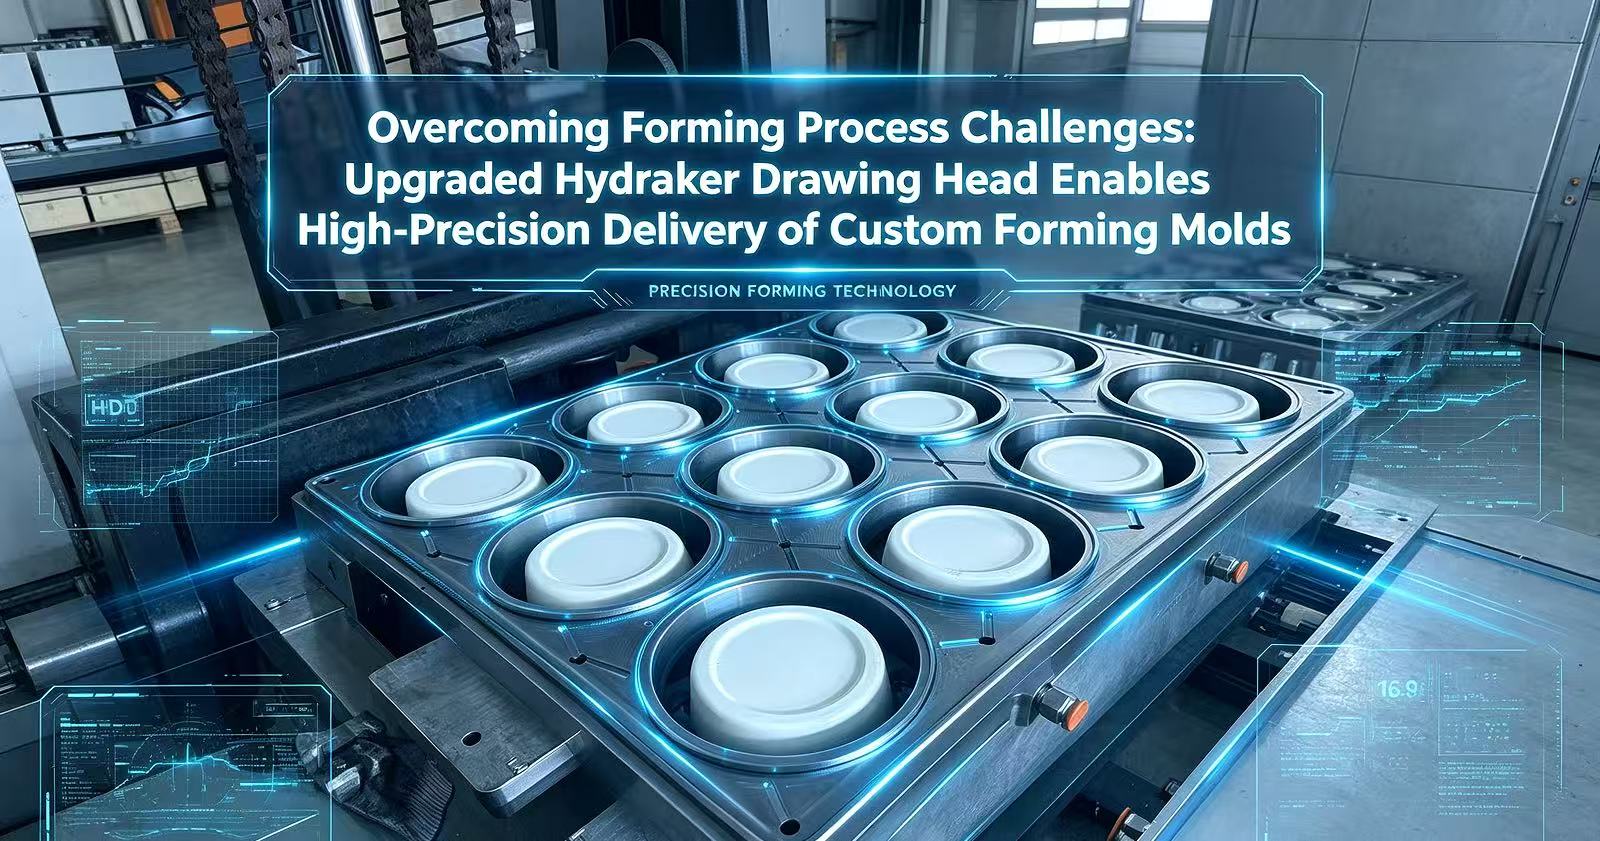
Whether the mold surface is smooth or not has a close relationship with the roughness of the product surface. Highly polished molds will produce products with a glossy surface, and dark molds will produce dull products.
Due to the different properties, especially the different thermal strength and tensile strength of plastics and the bonding characteristics of the plastic itself on the die surface, the requirements for the die surface are not the same. For example, polyolefin plastics such as polyethylene and polypropylene are quite difficult to form on the optical slip surface, so the surface of the Thermoforming mold used for this plastic should be appropriately roughened.
The best molding effect is to sandblast the mold surface. If the surface is too smooth, the gas can not escape from the mold and the material, which will cause the product to produce pinch, gas ring or ripple marks; If the surface is too rough, the surface of the product will not appear smooth, but also make the material flow difficult.
Hand file can be used to file on the side of the mold where the plastic flows along the direction of the plastic flow to make it rough. For high-precision positive molds, corners can be polished. The friction coefficient obtained will affect the wall thickness of the product. Where there is no air pinch, polishing can be done. The clamp of transparent products must be removed. Transparent products made of sheet metal, preferably with rapid reverse suction mold assisted molding. If this is not possible, the mold must be polished. The transparent zone in the product can also be formed by purposeful use of weak suction, but it is generally not used due to the uncertainty of cooling time, curling or deformation of the product.
Wooden molds can not be painted or painted, because the paint layer is easy to flake and break, and the smooth surface will lead to clamping, and the flow of materials on it is not good.