

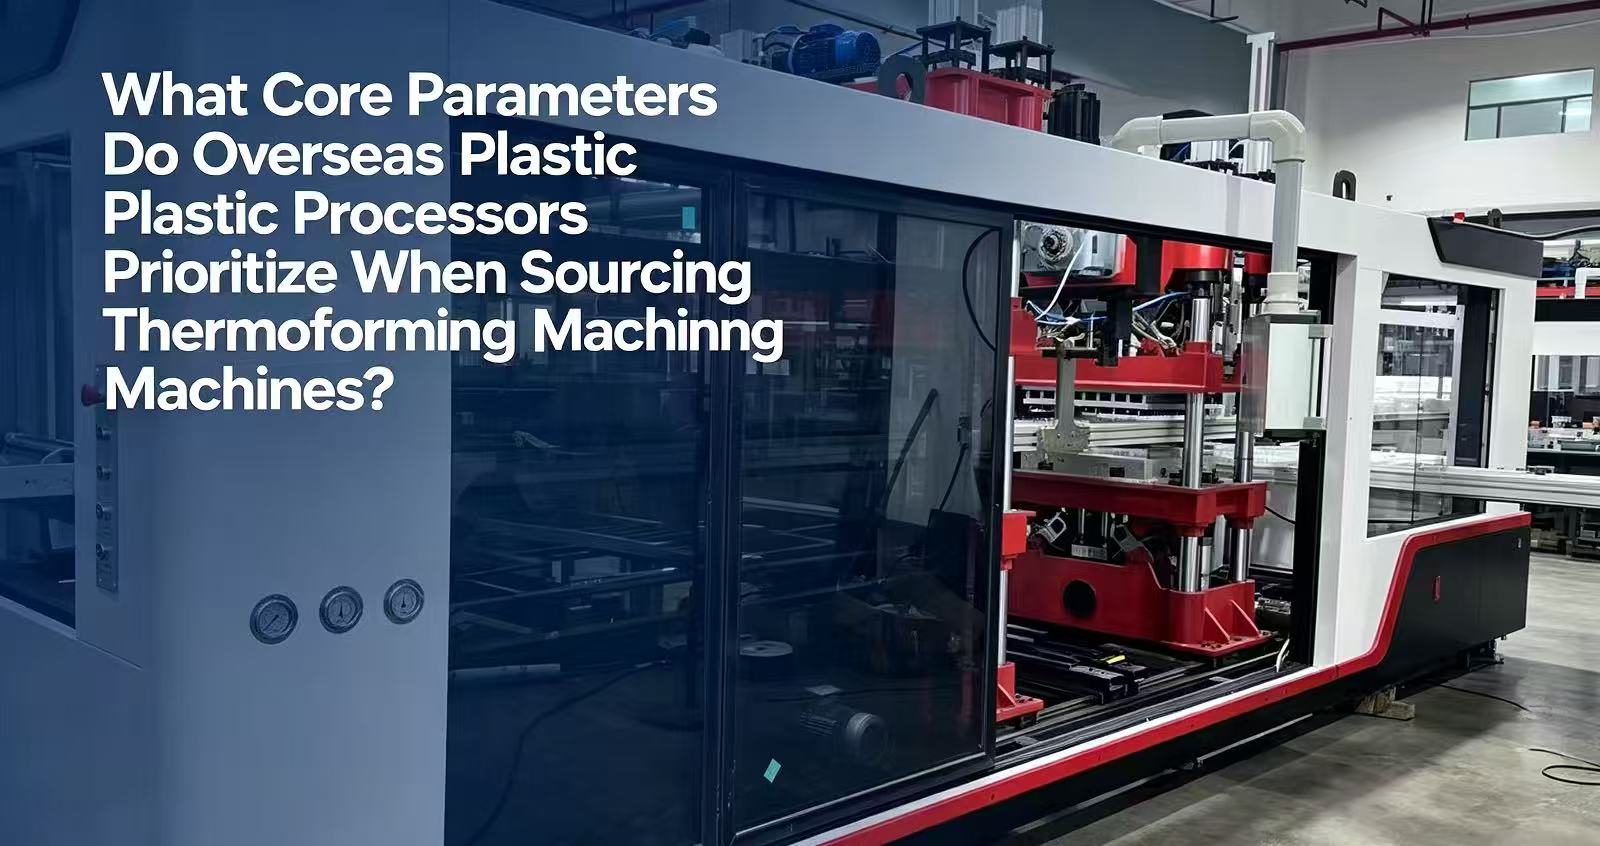
What are the Core Factors Foreign Plastic Processors Look for When Purchasing Thermoforming Machines?
1. Production Output and Cycle Time
Output is frequently the first parameter discussed because it has a direct impact on the abilities of the processor to fulfill customer requests. Nevertheless, the maximum speed a machine can achieve is different from its actual production output.
The complete production cycle, consisting of sheet loading, heating, forming, cooling, demolding, trimming, stacking, and any transfer time between operations must be evaluated in its entirety by the buyers. The most informative number that should be considered is the anticipated good part output in the normal conditions of operation instead of the maximum speed recorded during a short demo.
A practical production calculation is:
Good parts per hour = cycles per hour × cavities per cycle × equipment availability × yield rate
For instance, a machine that operates at 30 cycles each minute with four cavities per cycle, an 85% availability rate, and a 98% yield will yield approximately 6,000 acceptable products. This information is much more useful than just stating 30 cycles per minute.
Overseas processors usually ask suppliers to provide:
| Production parameter | Why it matters |
|---|---|
| Nominal cycle time | Shows the theoretical time required to complete one forming cycle. |
| Actual good-part output | Reflects cavities, uptime, rejects, and normal operating conditions. |
| Changeover time | Determines how efficiently the machine can handle multiple products. |
| Startup and stabilization time | Influences daily productivity and material waste. |
| Maximum machine availability | Helps estimate whether the system can support delivery commitments. |
Customers should also check if the mentioned cycle time pertains to any particular material, thickness, mold, and product geometry. Cycle durations may vary considerably from the given quote in case of using components with high deep draw, thick cross-section, sharp corner, or complicated cooling requirements.
2. Forming Precision and Product Consistency
Getting the exact shape is both important for products themselves and the ways they are combined with lids, inserts, machines used for filling, sealing and assembling. Incorrect wall thickness and geometrical variation can lead to leaky products, products that don't look nice, fragile corners and production interruptions.
In assessing the accuracy of forming, processors need to take into account factors beyond the stated positioning resolution of the machine. The final part is impacted by sheet temperature, heating uniformity of the sheet, mold design, vacuum performance and plug-assist timing, cooling effectiveness, clamping rigidity, and the shrinkage of the material.
3. Material Compatibility and Sheet Handling
A thermoForming Machine must be chosen based on the materials that will be utilized in practice, rather than merely those that are stated in the brochure. Some of the common materials used in thermoforming are PET, PP, PS, HIPS, ABS, PVC, PLA, CPET, APET, and multilayer or recycled sheets.
Different materials have distinct heating window, molding behavior, cooling requirements, shrinkage properties, and moisture sensitivity. Some processes require a certain level of recycled content or compliance with food contact regulations which affect the consistency of the manufacturing process.
Buyers should confirm the machine’s acceptable range for:
| Material consideration | Recommended information to confirm |
|---|---|
| Sheet type | Compatible polymers, multilayer structures, recycled grades, and bio-based materials. |
| Sheet thickness | Minimum and maximum thickness that can be heated and formed reliably. |
| Sheet width and length | Maximum usable sheet size and compatibility with existing suppliers. |
| Roll-fed or sheet-fed operation | Whether the system matches the processor’s material supply method. |
| Regrind or recycled content | Whether the forming process remains stable at the intended recycled percentage. |
The sheet feeding accuracy is also a significant factor. Misalignment can lead to less efficient utilization of materials and uneven formation within each cavity. Developing a sturdy clamping and indexing system helps improve the steady functioning of the machine.
4. Forming Method, Vacuum Performance, and Plug Assist
The forming technique must correspond to the shape and quality requirements of the product. Simple Vacuum Forming can be enough for simple packaging or shallow trays. Advanced techniques such as pressure forming, plug-assisted forming, or both may be required for deeper products, products with sharp details, sophisticated surface finishes, controlled wall thickness, etc.
A vacuum pump's performance is influenced by more than just its nameplate specifications. The entire system is comprised of factors like air passage within the mold, valves, piping, sealing surfaces, and the capacity and speed of the tank. A well-managed air system facilitates efficient removal of air bubbles and enhances accuracy in details.
For deep-draw products, plug assist is very significant. Plug design, material, temperature and timing influence distribution of materials. A well-designed plug helps mitigate excessive thinning on corners and achieve uniformity across all cavities.
To carry out an assessment of the technology, request the manufacturer to show the formation of the most complicated product in the selected category. The machine that successfully shapes a shallow simple part may not yield the same results when it comes to deeper containers or parts with various complex ribs or undercuts.
5. Mold Size, Forming Area, and Tooling Flexibility
Calculating the space available for forming indicates how many parts can be formed in one cycle and if there will be enough space for future product iterations. Buyers should evaluate the maximum mold size, useful forming area, maximum forming depth, mold height, and amount of clamping pressure.
Flexibility of the tooling is also crucial for the processors who need to work with multiple clients. A machine with fast mold change capabilities and interchangeable connections, recipe storage, and compatible mounting of the mold can shorten downtime.
Prior to buying, check whether the vendor offers assistance in mold design or collaborates with licensed tooling companies. The mold should be suitable for the vacuum channels, the cooling loop, plug-assist technology, trimming technique, and product discharge process of the machine.
6. Automation and Integration with the Production Line
Numerous foreign manufacturers are not considering to purchase a standalone former since they are either constructing or upgrading their entire production facility to include s.sheet feeding, preheating, forming, trimming, punching, stacking, marking, testing, conveying, granulating, and packing systems among others.
It is essential that the thermoforming equipment must do well in the communication with the systems. Different key integration points are electrical connections, communication protocols used, height of product transfer, production speed, rejected products disposal, access to the mold change, and safety interlocks.
Applications that involve accurate movements of sheets such as indexing, moving the plug, making cuts, or stacking items often rely on servo driven motion. While the introduction of automation increases the consistency of operation and reduces labor costs, it is essential to have trained personnel in control technology and access spare parts.
When requesting quotations, customers must be specific about what is included. A machine may be promoted as automatic although it still may require certain operations to be manually performed, for example trimming, gathering products, or dealing with scrap. The scope of the quotation should enumerate all additional equipment, sensors, conveyors or safety devices that are included in the order.
7. Trimming, Cutting, and Scrap Management
The quality of trimming can be considered as significant as the quality of the forming process for various packaging as well as industrial applications. The cutting machine is to provide sharp edges, accuracy in dimensions and operation at requisite speed without any damage to the product.
In choosing the method for trimming, processors should compare in-mold trimming, offline trimming as well as die cutting and CNC routing to determine what will be the best alternative. Such processes as in-mold trimming encourage reduced handling and more effective integration, while offline methods remain **better option** for small batches and complicated shapes.
Another factor to verify in equipment examination is waste recovery. Wastage and unacceptable materials may be ground and sent back to the production line, depending on the type of raw material and products produced. The supplier needs to explain how waste materials are removed from the system, if the pre-grinding machine is built in and how recycling affects the production control.
8. Controls, Data, and Operator Usability
An up to date control system is meant to make it easier to repeat the process, troubleshoot, and optimize it. A clear interface can show temperature zones, stages of the cycle, vacuum and pressure, the position of servos, alarms, total production, as well as maintenance reminders.
Recipe management becomes very useful in situations when a processor is producing many different products. An operator has to be able to save and recall validated settings for heating, shaping, cooling, cutting, and stacking. Password permissions can allow for prevention of unauthorized adjustments to important parameters.
Data originating from production helps far-reaching enhancement. The types of vital information include current cycle time, reasons for downtime, number of rejected products, energy usage, alarm history, and output per shift. Depending on the situation, remote diagnostics cut down response time; however, buyers must verify the cybersecurity procedures and check whether they can exercise control of remote access and decide on its use.
The training for operators should encompass normal functioning procedures, adjusting the recipe, changing the molds, clean-up, troubleshooting, and safe maintenance procedures. The best interface must not only be sophisticated but also be easily comprehensible to the users.
9. Reliability, Maintenance, and Machine Construction
A thermoforming machine’s reliability is one of the most important aspects of its actual worth. To evaluate a thermoforming machine, potential buyers should assess its frame, clamping system, drive mechanism, heating element, pneumatic systems, lubricant points, and service accessibility.
A stiff structure ensures constant forming and cutting accuracy. Industrial heavy-duty guide rails, bearings, servos, valves, heating devices, and sensors can help reduce unexpected downtimes if selected and used properly. However, product quality should be analyzed with the engineering and servicing abilities of the manufacturer.
10. Safety and International Compliance
Safety criteria change according to the location but it’s common that overseas customers check whether the machine has monitoring over the guards, emergency stop system, electric shielding, access doors, burning surface alarms, pneumatic safety systems, and documentation.
Depending on the target market, an equipment may have to meet requirements with respect to CE marking as well as UL components, local electrical codes, or national standards. The compliance should be ensured at the quotation and design stages rather than after the machine has been completed.
Sources should consist of electrical schematics, pneumatic diagrams, risk-assessment information, the operating instructions, maintenance procedures, lists of spare parts, and, where relevant, conformity declarations. Clear documentation is helpful for safer installation and can facilitate local inspections.
11. Total Cost of Ownership and Return on Investment
Price at purchasing is only one portion of investment. Accurate cost analysis should cover machinery, molds, useful equipment, installation, transportation, installation, education of operatives, energy, labor, maintenance, spare parts, material waste, and probable downtime.
Processors could leverage the possible cost per good part produced by a supplier as an evaluation measure. This figure must also consider the assumptions for output, yield, electricity, labor, mould life, maintenance, and yearly hours of operation. Even if the purchase price of a machine could be a little bit higher, it may show a lower cost per part made if it is characterized with a better operating time, lower level of scrap, quicker changeovers, and higher energy efficiency.
Please send an estimate showing which features are standard and which ones are optional. It is important to determine if the price includes shipping to the port, installation supervision, training of the operator, testing of the equipment, warranty and updates to the software.
12. Supplier Experience and After-Sales Support
When deciding to buy a machine, customers must also assess the experience of the supplier in dealing with similar materials, applications, and quantities.
It is important for a legitimate supplier to discuss both process limitations and benefits. Request for references from the customer for similar products, samples of parts manufactured from similar materials, and an overview of standard commissioning process. A conversation limited only to speed and price may not tell you about the adequacy of the machine for your requirements.
Prior to signing the contract, outline the acceptance test, guarantees regarding its performance, warranty period, response time, extent of training, responsibilities for installation, and procedure for dealing with non-conforming items. These points help avoid misunderstandings and provide a level of verifiability before the final approval.
How to Prepare a Strong Thermoforming Machine Inquiry
The proposal quality presented by the supplier largely relies on information received from the buyer. The more comprehensive the inquiry, the more likely the supplier is to suggest the appropriate configuration of machines instead of recommending a standard product.
| Information to provide | Examples |
|---|---|
| Product details | Drawings, dimensions, weight, wall thickness, tolerances, surface requirements, and photographs. |
| Material details | Polymer type, sheet thickness, sheet width, recycled content, and expected material changes. |
| Production target | Required parts per hour, working days, shifts, annual volume, and expected peak demand. |
| Tooling information | Number of cavities, mold dimensions, mold material, cooling method, and whether a new mold is required. |
| Factory conditions | Electrical voltage and frequency, compressed-air pressure, cooling-water conditions, floor space, and local regulations. |
| Automation requirements | Stacking, trimming, inspection, scrap recycling, packaging, and connection to existing equipment. |
Furthermore, it is crucial to pinpoint the most challenging product in the envisaged portfolio. This allows the supplier to propose a machine that meets the greatest technical requirements instead of simply recommending the machine that makes the least complicated parts.