

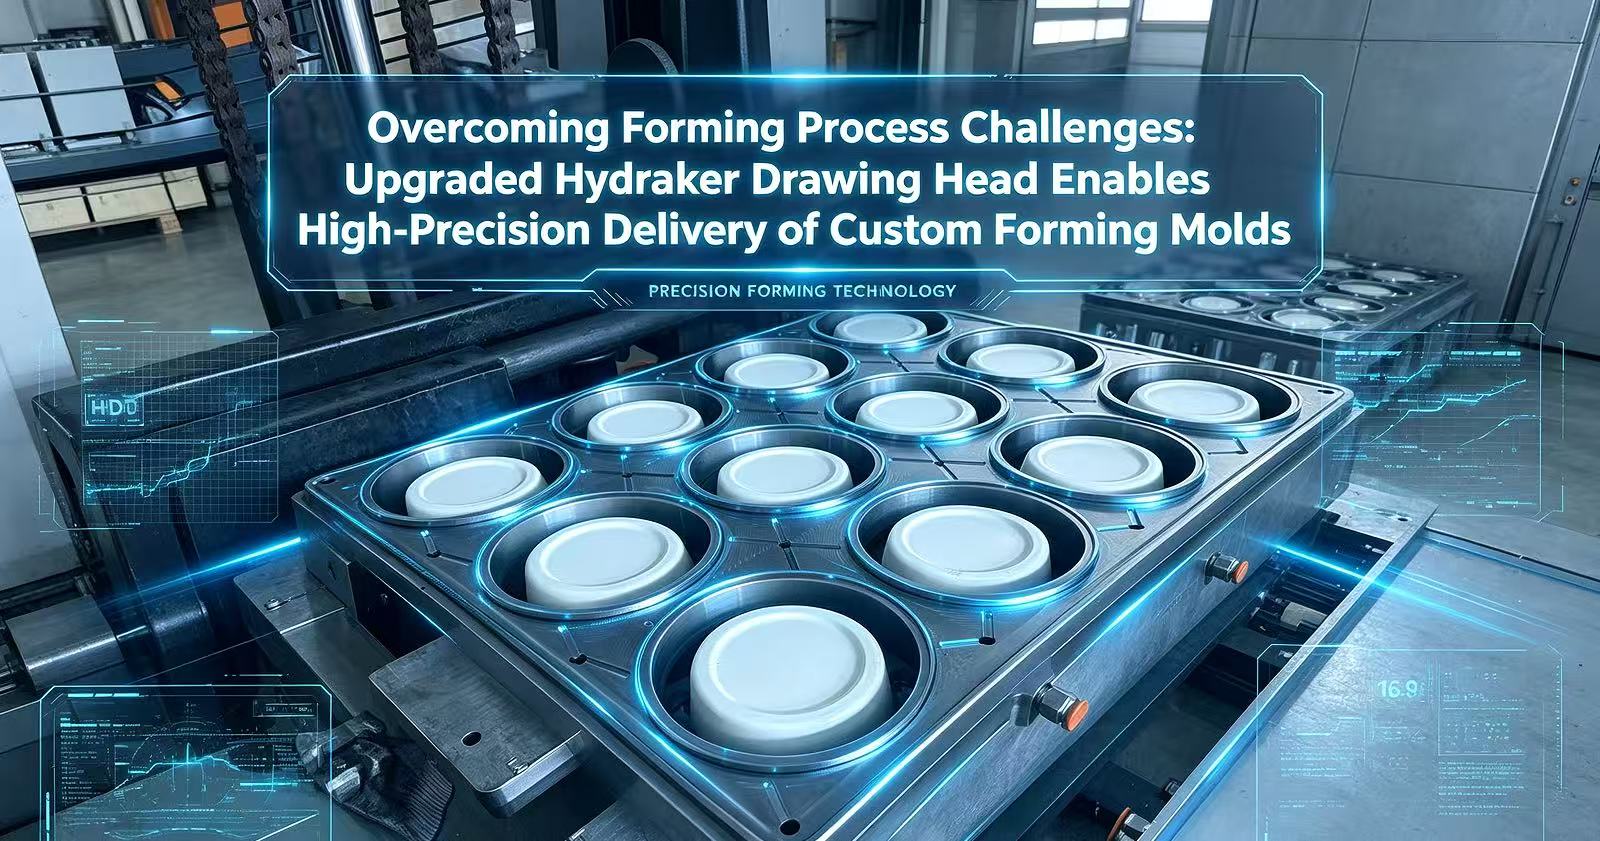
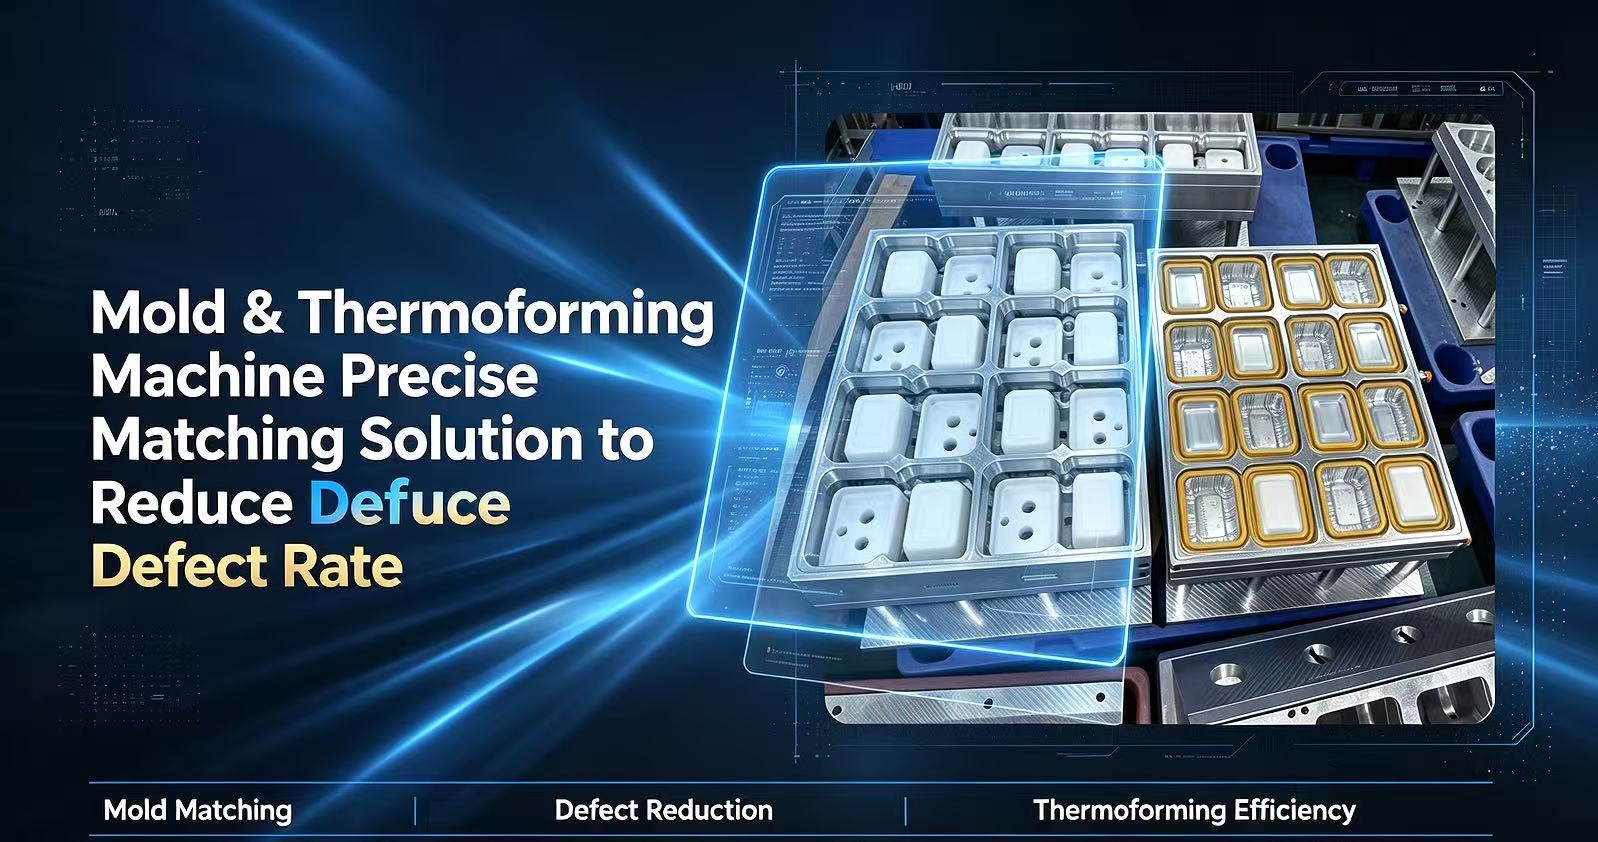
Solving Difficulties that Face Forming Processes: Hydraker Drawing Head Has Been Upgraded to Aid in Accurate Delivery of Custom Forming Molds
Common Problems in Precision Forming
Manufacturers should pay attention to the following signs:
Inaccurate punching positioning: The material does not enter the mold at a consistent reference position.
Dimensional deviation: Critical dimensions vary between parts even when the mold and material remain unchanged.
Forming wave pattern: Wrinkles or waves appear on flat surfaces, sidewalls, or transition areas.
Uneven wall thickness: One area becomes thinner because the material is drawn unevenly.
Unstable production rhythm: The process works at low speed but becomes unreliable during continuous or high-speed production.
Why the Drawing Head Matters
The head of the drawing device regulates the entry and movement of the sheet through mold systems. Any mismatch of its design with the forming method can lead to uneven pressure, lateral displacement, vibrations, or irregular flow of the materials.
In this case, just changing the die may not help address the core issue. The die could be made the right way, but the machinery interface could prevent it from reaching the desired accuracy.
It is for this reason that mold technical optimization has to involve the assessment of the design head, the feeding precision, the alignment of equipment, the molding force and the process timing.
How a Hydraker Drawing Head Upgrade Improves Performance
More balanced forming force
A new drawing head can spread the forming force more uniformly over the working area. This approach minimizes uneven stress, patches of buckling, excessive thinning, and lateral damage.
Improved material positioning
Better guidance and support will ensure that the sheet enters the mold in the same position every time, which is especially important in the case of special molds with small tolerances and complicated designs.
Better feeding and forming synchronization
Activities such as feeding, clamping, drawing, release and return should be performed in the correct order. By fine-tuning the drawing-head construction and the control timing, a sudden movement of the material can be minimized, thus improving the repeatability.
Higher structural stability
If the head of the drawing process is deflected by the pressure of the work, the actual position of molding may vary from the finding made while setting up. Improving the rigidity of the structure will assist in keeping the position aligned during the stroke.
Controlling Punching Deviation and Surface Waves
In order to minimize variation in punching precision, manufacturers must implement a reference framework and carry out a series of measurements on a sample of production batches. A consistent deviation may suggest that the equipment may not be properly aligned, while irregularities may indicate issues with feeding, vibrations, or inconsistency in the clamping force.
In order to understand a wave formation, an engineer has to look at:
- Drawing force
- Material flow
- Lubrication
- Die clearance
- Forming speed
- Blank-holder pressure
An upgrade on the drawing head is going to stabilize force and movement but in order to have the complete forming process checked.
Once renovation is complete, the original and improved outcome must be compared through the same mold, material, machine settings, and method of inspection. Dimensions, surface quality, speed of production, frequency of adjustment, and yield are the major indicators.
Recommended Optimization Process
A practical technical renovation normally follows these steps:
- Review the part drawing, mold structure, material specifications, and current production data.
- Determine where the primary problem arises from: alignment, distribution of force, feeding mechanism, timing or the mold situation.
- Design the drawing-head modification according to the actual forming requirements.
- Install and adjust the upgraded structure while checking guides, sensors, and safety functions.
- Confirm the result using dimensional inspection, surface inspection, as well as constant trial manufacturing.
The manufacturer is thus able to enhance the entire equipment set rather than depending on the repeated adjustment by the operator.
Frequently Asked Questions
How is it possible to increase the equipment flexibility, avoid the forming flaws, enhance the cavity quality and overall productivity, and satisfy high-precision mass-production custom requirements with the help of a renovation of the special drawing head?
The initial stage of the entire process involves thorough examination of the machine, molds, material, feeding system, molding cycle, and manufacturing pace. Then engineers make the necessary optimization of the structure of the drawing head, guiding method, force distribution and operations, considering customers’ wishes.
When the installation is complete, the results are checked through dimension measurement, repeatability tests, inspection of surface quality, and production tests. It leads to reduction in positioning mistakes, wave formation, adjustment time, and number of rejected products while ensuring good consistency during mass production process.
Should the mold be replaced if forming defects continue?
It isn't always true. If the mold has a correct shape, but the process experiences unstable positioning, uneven force, or disparate results depending on the production speed, it is likely that the drawing head or equipment interface is to be blamed. If the mold is faulty due to incorrect shape, excessive wear, or incongruous design parameters, the mold will need to be replaced.
What information is needed for a drawing-head optimization project?
Helpful materials comprise drawings of parts and molds, specifications of materials, machine models, production speed forecasts, defect images, and reports on measurement characteristics associated with machines as well as operating parameters. Such complete information lets the technical team estimate the scope of reconditioning accurately.
Conclusion
The cooperation of the various components such as the mold, machine, material, feeding system, and drawing head plays a significant role in making the forming process a high-precision process. When there are problems with positioning accuracy, dimensional deviation, and the appearance of the forming wave pattern, it is more advantageous to upgrade the Hydraker drawing head instead of simply replacing the mold. By using balanced force transfer, precise guidance, better synchronization, and structured validation, a manufacturer may enhance their forming consistency and production efficiency.